
The ideal moisture content for acacia exports is usually **8% to 12%**, depending on whether the product is indoor furniture, outdoor furniture, panels, or components. Exporters in Thailand
Common buyer target for exported indoor acacia furniture: **10% to 12% moisture content** at final inspection.
That target matters because acacia remains hygroscopic after kiln drying. It will still exchange moisture with surrounding air during storage, container loading, ocean transit, and installation. Guidance from the **USDA Forest Products Laboratory** and practical furniture manufacturing standards both show that moisture mismatch drives movement, including swelling, shrinkage, cracked joints, and finish stress.
For most exported acacia furniture and components, **8% to 12% moisture content** is the practical target, while **10% to 12%** is common for indoor furniture. The right number depends on destination climate, product construction, and packaging time, but shipping above 12% usually increases the risk of movement, mold, and claims.
A simple rule is to match the wood as closely as possible to the equilibrium moisture conditions expected at the destination. Indoor furniture shipped to the **United States**, **Europe**, or climate-controlled commercial projects is often specified at **10% to 12% MC**. Smaller components, laminated parts, and joinery stock may be held slightly tighter because thin sections react faster to humidity swings during warehousing and installation.
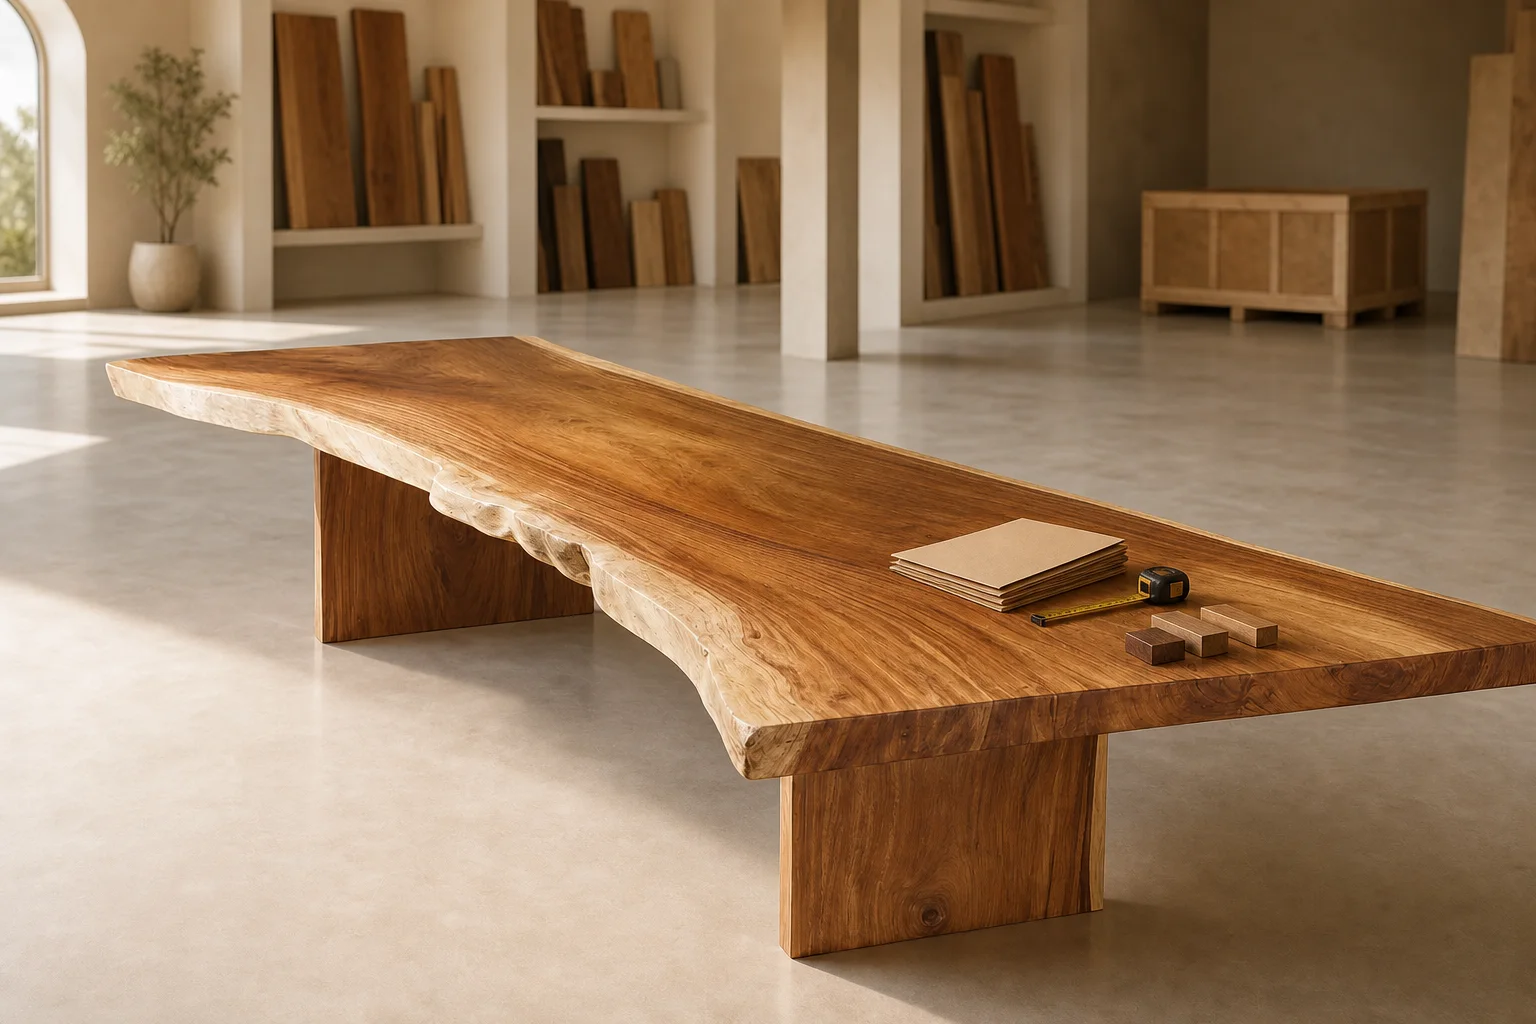
Moisture content matters because acacia continues to gain or lose water after production, and even a few percentage points of mismatch can change dimensions, stress joints, and damage finishes. For exporters, correct moisture content lowers rejection risk, supports dimensional stability, and helps products perform predictably after long container transit.
Acacia is dense and attractive, but like **teak**, **oak**, and other hardwoods, it moves when ambient humidity changes. If wood leaves the factory too wet, panels may shrink after arrival, creating gaps, checks, or loose joinery. If it is too dry for the destination, parts can swell later. The **USDA Forest Products Laboratory** explains that dimensional change is a direct function of moisture change below fiber saturation.
Export conditions add more variables than local delivery. A container may move from **Bangkok** production, to port storage, across ocean routes, and into air-conditioned interiors. Each step changes relative humidity and temperature. That is why buyers often ask for meter readings, kiln records, and spot checks on concealed areas before approving shipment.
Yes. The ideal moisture content for acacia exports changes with end use, section thickness, and destination climate. Indoor furniture for dry, climate-controlled interiors usually needs tighter control than outdoor pieces, while thick slabs or tabletops often require slower conditioning and closer monitoring than smaller machined components.
{'type': 'table', 'caption': 'Typical acacia export moisture targets by application', 'headers': ['Product or destination context', 'Typical target MC', 'Reason'], 'rows': [['Indoor furniture for climate-controlled interiors', '10% to 12%', 'Balances stability during shipping and indoor use'], ['General finished export goods', '8% to 12%', 'Broad practical export range'], ['Outdoor furniture or semi-exposed use', '10% to 14%', 'May tolerate slightly higher ambient exposure'], ['Thick tops, slabs, or large panels', 'Often held near 8% to 10% core-to-surface consistency', 'Reduces differential movement and checking']]}
Destination climate matters because equilibrium moisture content differs between dry interiors and humid tropical settings. Product type matters because a chair rail, laminated leg, and solid tabletop do not behave the same way. Export specifications should therefore state the moisture target, test method, sampling points, and allowable variation between pieces rather than relying on one blanket percentage.
Acacia moisture content should be measured with calibrated pin or pinless moisture meters, verified on representative samples, and recorded close to packing time. Good practice includes testing multiple locations on each piece, checking thicker sections separately, and confirming that surface readings align with internal moisture after conditioning.
A single reading is not enough. Quality teams typically test faces, edges, rails, legs, undersides, and thicker parts because moisture can vary within one item. Pin meters can help identify localized wet spots, while pinless meters speed up screening across larger volumes. Meter species settings, depth limits, and calibration should be documented so readings are interpreted correctly for acacia density and thickness.
{'type': 'image', 'src': 'https://mfurniturethailand.com/images/resources/acacia-moisture-meter-inspection.jpg', 'alt': 'Acacia furniture component moisture meter inspection before export packing in Thailand factory', 'caption': 'Pre-shipment moisture checks should sample multiple locations and thicknesses, not only visible surfaces.'}
Many buyers also request testing after final machining and after acclimation in finished-goods storage, since fresh cuts can expose wetter cores. If readings are clustered within the specified range and the factory maintains stable storage conditions, the shipment is less likely to develop surprises during transit or installation.
When exported acacia is too wet, it may shrink, cup, split, mold, or loosen at joints after arrival. When it is too dry, it can absorb moisture later, swell, and stress assemblies or finishes. In both cases, the result is instability, rework, claims, and lower buyer confidence.
Over-wet acacia is the more common export risk because the problems often appear only after unloading. Typical symptoms include open glue lines, sunken panels, end checks, rough grain raising under finish, and visible shrinkage around mortise-and-tenon joints or hardware. Excess moisture can also increase mold risk if products are packed with limited airflow or exposed to condensation during container transit.
Over-dry stock creates a different problem set. Once installed in a more humid environment, parts may expand, bind, or telegraph stress under coatings. The goal is not the lowest reading possible; it is the correct reading for the destination and construction method. That is why exporters, inspectors, and buyers should evaluate moisture content together with machining, joinery, and storage controls.
Buyers should ask for the target moisture specification, meter type, calibration method, sample size, reading locations, and final inspection date near loading. They should also request evidence of kiln drying, conditioning, and storage control, because acceptable moisture content is meaningful only when supported by consistent handling and documentation.
For higher-value programs, buyers may also specify third-party inspection or AQL-based sampling before shipment. That is especially useful for hospitality, retail chains, or custom projects where replacements are expensive. Clear moisture specifications prevent disputes because both parties can compare readings, sampling methods, and tolerances against a written standard rather than against assumptions.
Not necessarily. **8% MC** can be appropriate for some acacia components, panels, or destinations, especially where interiors are dry and climate controlled. However, for many finished furniture exports, buyers prefer **10% to 12%** because it offers a practical balance between shipping stability, machining performance, and later in-room movement.
It can be, but **14% MC** is usually higher than ideal for many indoor export programs. That level may be more acceptable for certain outdoor or semi-exposed applications, yet it increases the chance of shrinkage, finish stress, and joinery movement after arrival in drier interiors or air-conditioned commercial spaces.
It should be checked at multiple stages, but the most important verification is close to final packing after machining, assembly, and conditioning are complete. Earlier kiln readings are useful, yet buyers care most about the moisture condition of the wood that actually enters the container and reaches the destination market.
Not always, but third-party inspection is helpful for large orders, hotel projects, retail programs, or first-time supplier relationships. Independent checks can verify meter settings, sampling points, and consistency across SKUs. They reduce disputes by documenting whether the shipment met the agreed acacia moisture range at the time of loading.
This resource is for general educational guidance and does not replace project-specific engineering, testing, or contractual specifications. Moisture targets for acacia exports should be confirmed with the buyer, factory, and inspection team based on product design, destination climate, and end use.
